
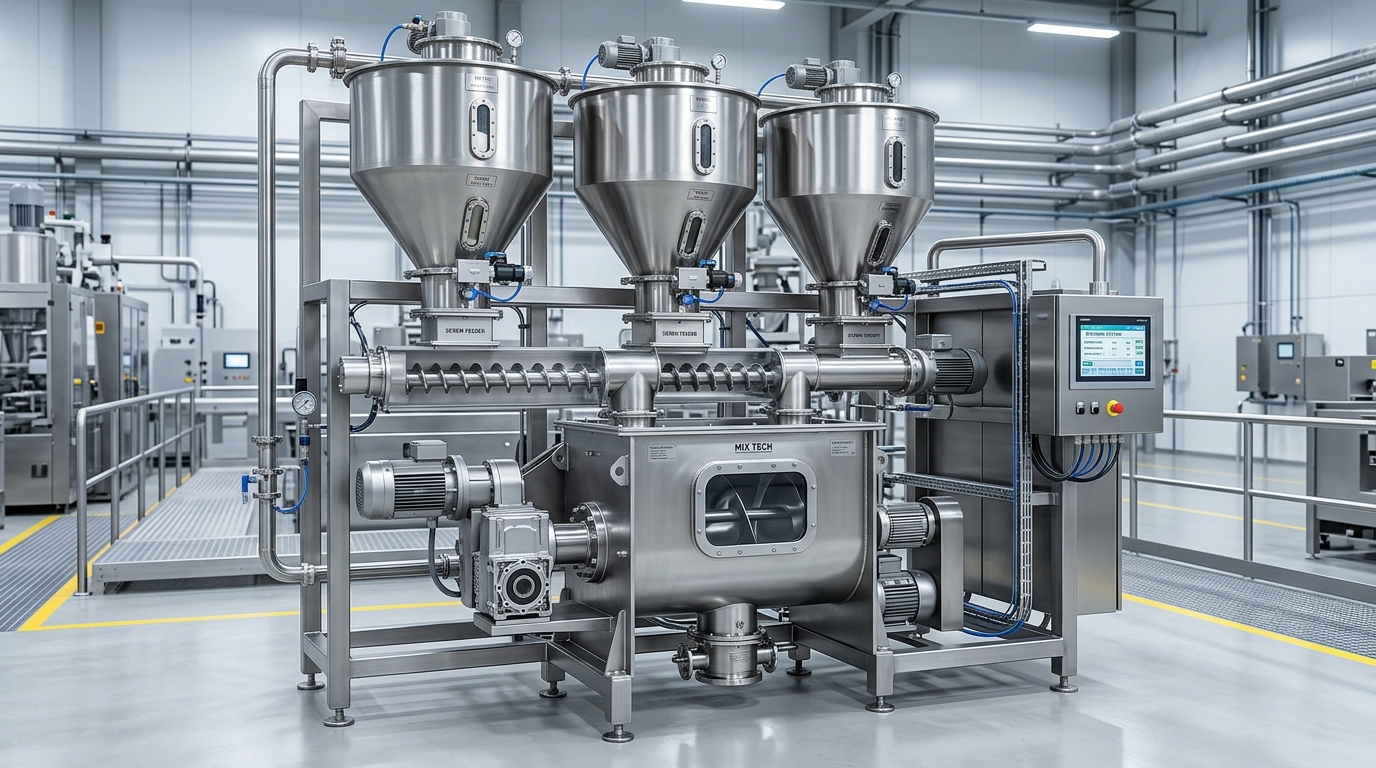
Engineered for continuous work in Chemicals & Petrochemicals facilities.
Chemical and polymer manufacturing environments present harsh operating conditions including corrosive fumes, combustible dust, and high product density. AXION PackTech manufactures heavy-gauge steel conveyors, dust-tight bulk bag fillers, and ATEX-certified packaging lines engineered for continuous 24/7 reliability.
Key Sector Challenges
Critical production and handling bottlenecks encountered in chemicals & petrochemicals operations.
Combustible dust explosion risks in bagging and conveying zones
Corrosive chemical powders degrading standard mechanical components
Dense material handling without line bottlenecking or motor overload
AXION Technical Solutions
Proven machinery, material flow controls, and automation architectures.
Explosion-Proof Packaging Systems
ATEX / PESO certified flameproof control panels, motors, and dust-tight bag clamps.
Corrosion-Resistant Conveyors
Heavy structural steel with epoxy coating or 316L stainless steel for acid/alkali resistance.
Measurable Commercial & Plant Benefits
Certified for hazardous Zone 1 / Zone 21 operations
Extended mechanical life in abrasive and acidic environments
Integrated aspiration hoods to maintain clean shopfloors
Common Applications
- Polymer Resins→
- Agrochemicals→
- Industrial Pigments→
- Specialty Chemicals→
Other Industrial Sectors
Food & Beverage
Sanitary stainless steel 304/316 bagging and automated pouch packing lines for food processors.
Explore →SectorPharmaceuticals & Life Sciences
Cleanroom-ready, cGMP-compliant rotary filling, capping, and sterile material handling.
Explore →SectorAgriculture & Seed Processing
High-throughput bagging, weighing, and palletizing conveyors for seeds, fertilizers, and crops.
Explore →SectorMinerals, Cement & Building Materials
Abrasion-resistant heavy conveying and valve bag filling systems for cement, sand, and minerals.
Explore →